Current plan
M-01 running
- Energy over 30 min
- 31.1 kWh
- Peak power
- 64.7 kW
Machine Monitoring
The gateway reads status from the PLC or digital inputs, and values from sensors on the machine, and sends them to the cloud — so you see which machine is running, which has stopped, and which value is starting to drift.
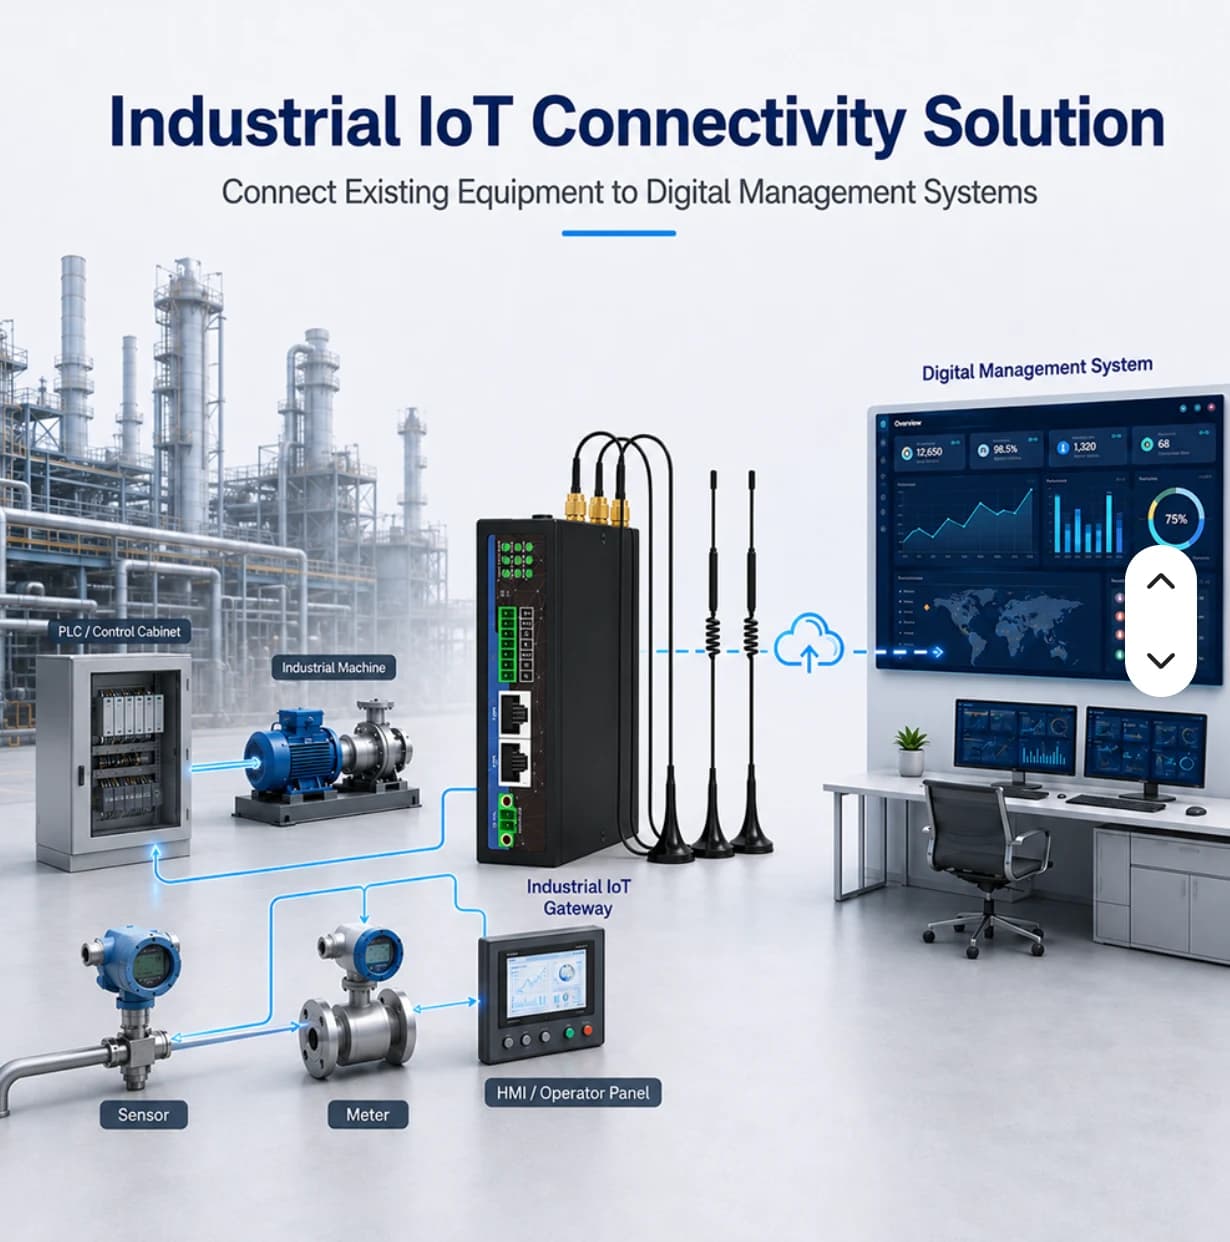
Read through the gateway, shown on the dashboard, with history charts.
These indicators are in development and will be enabled step by step. You can preview them in the demo.
From shop-floor equipment to dashboards and alerts.
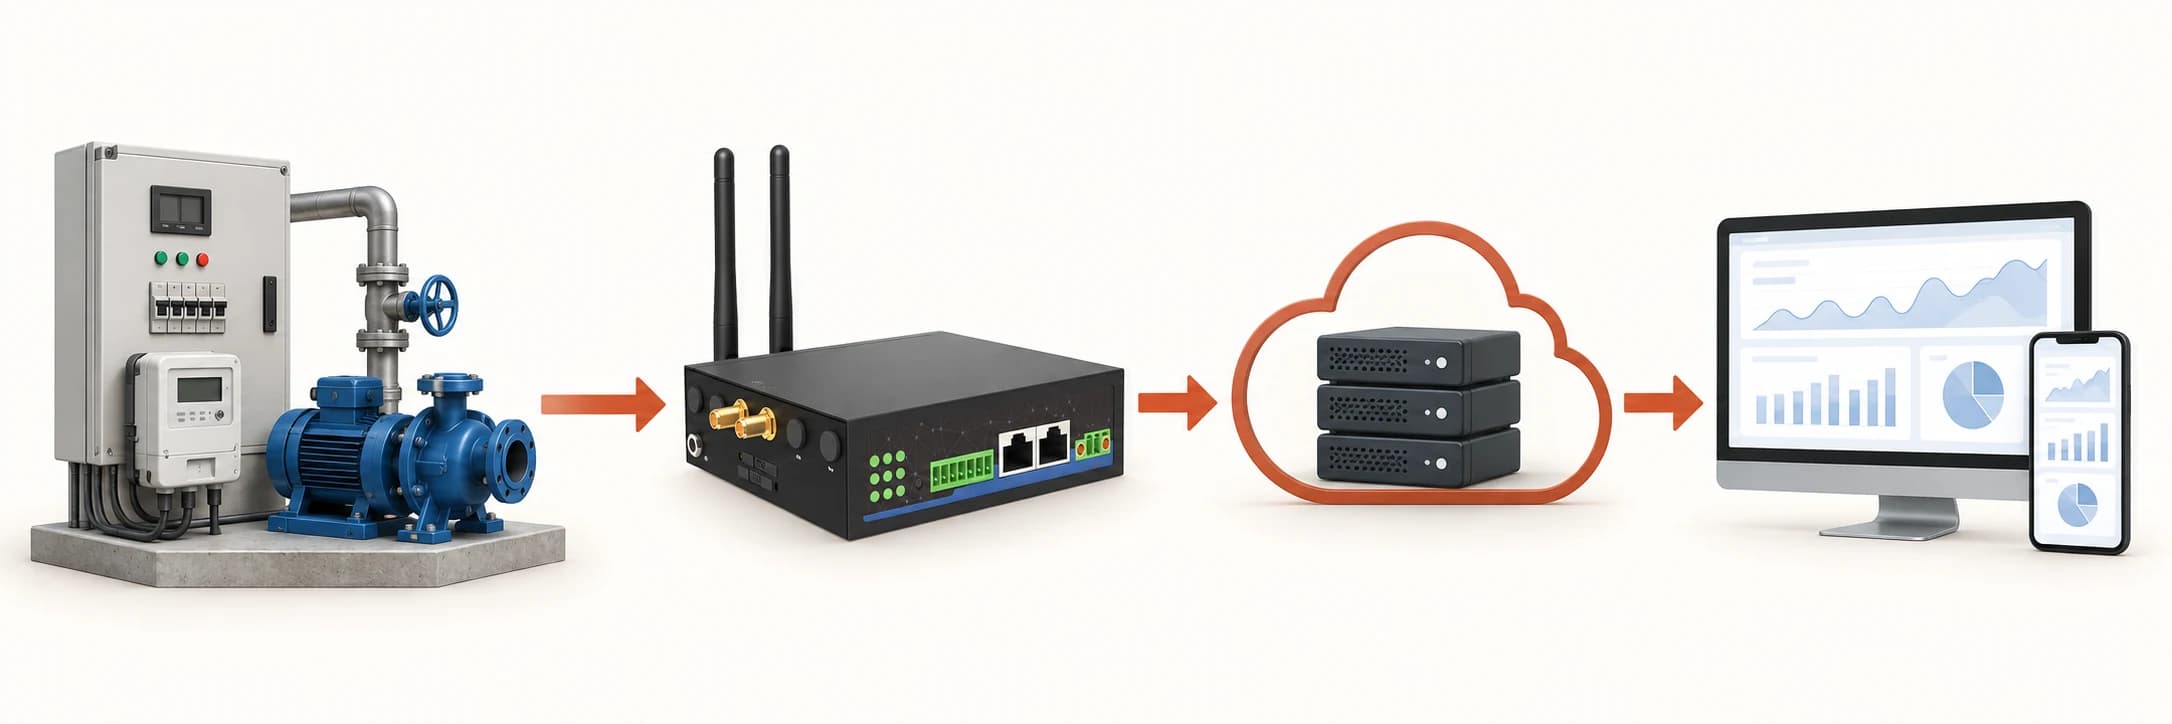
Scroll to explore the connection path →
The machine's PLC or added sensors
Modbus RTU / TCP or digital inputs
Reads values; buffers when the connection drops
Dual SIM or site LAN, encrypted with TLS
Time-series storage, isolated per organization
On the web; alerts via LINE and email
Available as soon as the gateway is installed.
Latest values and charts for every data point, on desktop and mobile.
Detailed data for 30 days on every package; longer history is kept as summarised data, by package.
Set a high / low limit per data point. When a value goes out of range, you are alerted via LINE and email.
Get alerted when a gateway or device stops sending data — no need to wait for someone to notice.
AI capabilities are on our roadmap. They are not available yet.
Example: surface vibration or temperature trends that drift from that machine's usual behaviour.
FACTORY APPLICATIONS
Illustrative system designs with equipment, data, responsible teams and project conditions. These are not customer case studies.
DIGITAL TWIN · SIMULATED
This simulated digital twin is a model running in your browser. It does not mirror a PLC or customer site and does not control equipment.
Live (simulated) · 08:00:00
Illustrative 3D layout, not surveyed coordinates. Scene labels show values from the simulated twin. Select equipment on the scene or in the twin tree.
WHAT-IF · SIMULATED
M-01 running
M-01 stopped
Computed from the browser simulation to compare choices; not a prediction for a real site.
Select a scene device, then inspect or control it
PLC / Meter → Modbus TCP / RS485 → Gateway → MQTT TLS :8883 → Monitor
CCTV uses IP over PoE / NVR independently of LoRaWAN. This scene is illustrative and has no live video.
Connect power readings and machine states to site locations for maintenance inspection.
Connect PLC or sensor signals so production and maintenance use the same observations before developing performance analytics.
This illustrative line has feeding, filling and packing stations. Start with run/fault states and counters exposed by the PLC. Existing controls are not automatically modified, and an offline gateway is not treated as evidence of a machine stop.
Shift leaders lack a shared view across multiple machines
Approach · Define readable PLC states and display them by machine with update timestamps
Investigations begin without reliable times and source signals
Approach · Retain relevant states and readings to identify investigation periods; a person still confirms the actual cause
A calculated number may not represent production correctly
Approach · Separate acquisition from analytics and define shifts, counts, good units and ideal cycle times before agreeing OEE formulas
Production and PLC owner
Agree run, stop and fault meanings, including changeovers and planned stops
Automation engineer
Document addresses, types, units and a read method that does not interfere with control
Installer and operator
Compare displayed states with machine behavior during an agreed test
Shift leader
Check states and freshness, using history to select periods for investigation
Maintenance
Inspect the machine and record causes through the factory process rather than assuming them from one signal
Production engineering
Validate counts, shifts and formulas before adding downtime or OEE analysis
Coordinate using station-level readings and event timestamps
Use historical signals as evidence rather than relying only on recollection
Maintain and extend the system using shared point definitions
Identify available and missing inputs before investing in performance analytics
DETAILS & PLANNING
Interpret run, fault and cycle-complete signals with the machine owner. No-work conditions, planned stops and communication loss may produce different data patterns. Do not label every gap or inactive signal as downtime without an agreed definition.
OEE needs planned production time, operating time, a reference production rate and good-unit counts. Status signals alone are insufficient. OEE and downtime analytics require confirmed feature availability and jointly agreed definitions.
Extend machine monitoring with SCADA, factory control and OEE, using RFID or barcode to associate events with jobs, lots and products. Define production inputs and separate readings from control commands.
Review each system’s scope before opening it or using the example to plan your project.
Simulated data · No physical PLC commands
Explore machine states, energy, simulated readings and alarms with a 3D scene and example event history.
Demonstration with simulated data
Explore energy, machine monitoring and OEE examples with a 3D factory to understand data and workflows before planning a project.
It depends on whether the required data is already exposed. The PLC owner should confirm addresses and access. Program changes must be a separately agreed scope.
No. Monitoring is not a safety control system, and Phase 1 does not write commands to field equipment.
The demo uses simulated data from a sample plant. Our team can assess your actual equipment and site.